

Excellent performance of large-load palletizing robots in practical applications
Release time:
2025-02-17
With the rapid development of logistics, warehousing and manufacturing, large-load palletizing robots are becoming indispensable and important equipment in modern industrial production and logistics due to their high efficiency, accuracy and reliability. Whether it is in the fields of food and beverage, chemical industry, building materials or e-commerce logistics, large-load palletizing robots have shown wide application value.
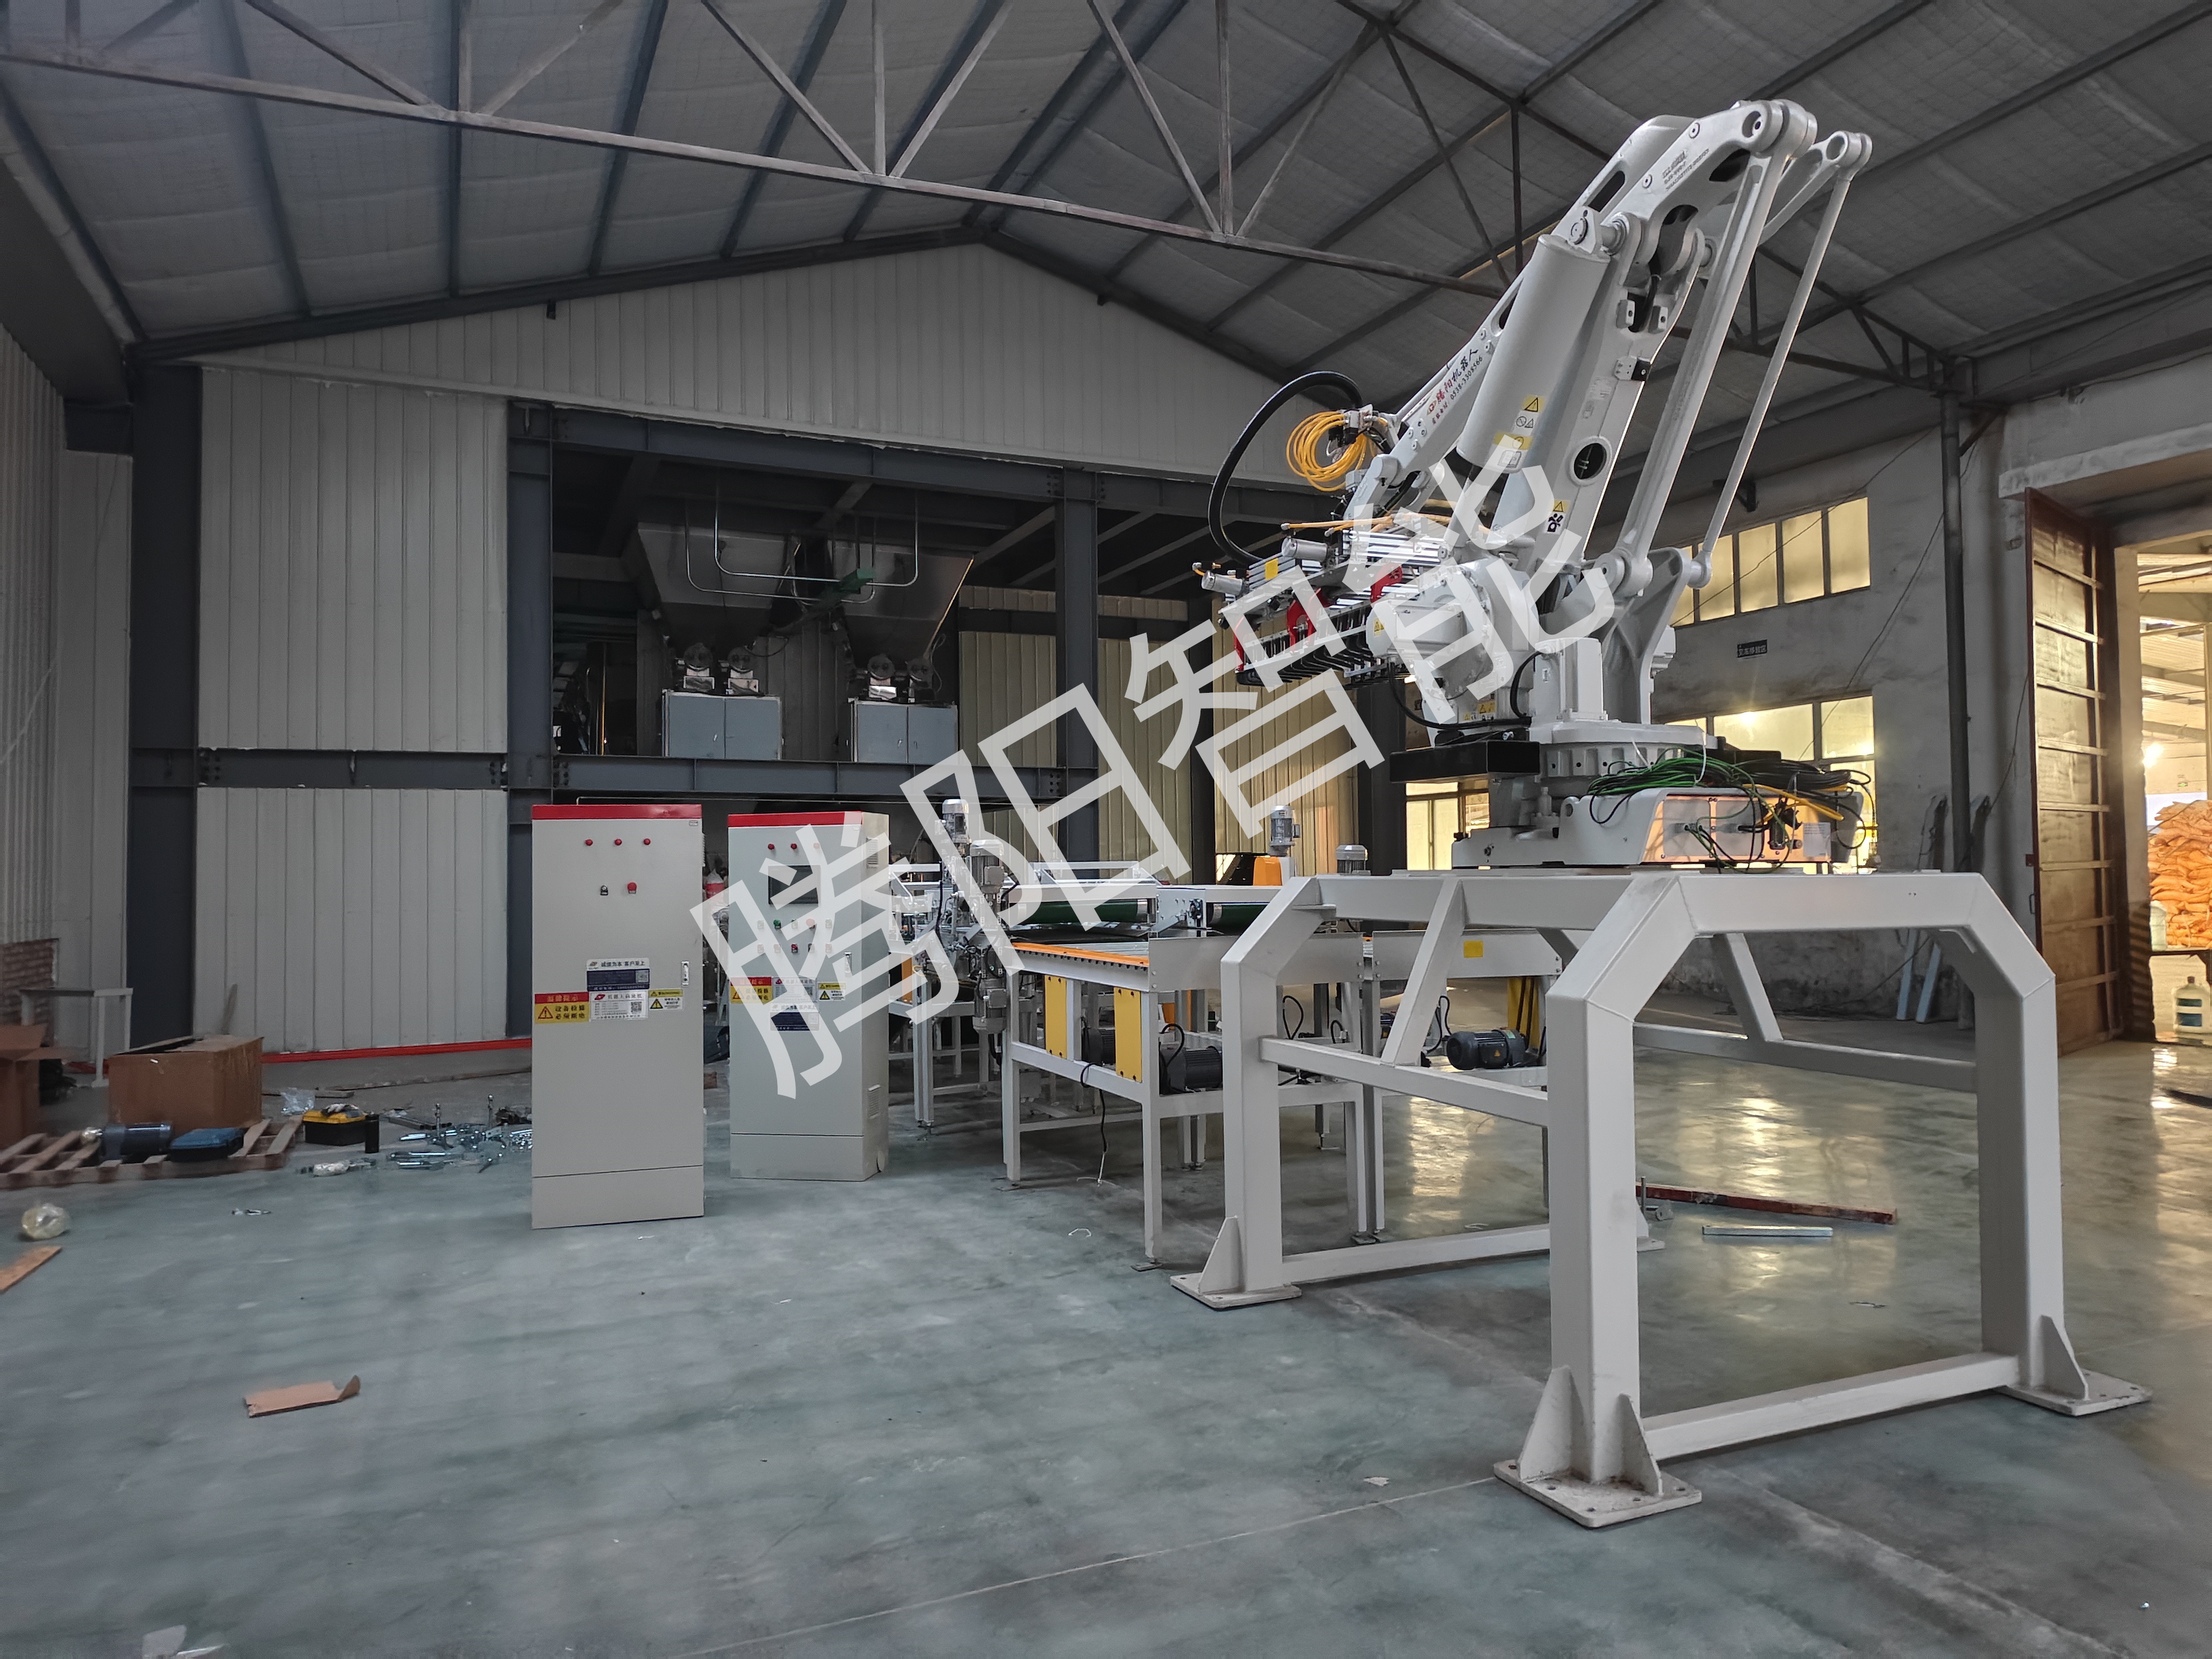
With the rapid development of logistics, warehousing and manufacturing, large-load palletizing robots are becoming indispensable and important equipment in modern industrial production and logistics due to their high efficiency, accuracy and reliability. Whether it is in the fields of food and beverage, chemical industry, building materials or e-commerce logistics, large-load palletizing robots have shown wide application value.
1. Core advantages of large-load palletizing robots:
High load-bearing capacity: It can easily carry heavy objects from 500 kg to 2000 kg, meeting the needs of heavy material handling.
High precision and stability: Adopt advanced servo control system to ensure precise positioning and stable operation during the palletizing process.
Efficient operation: able to work 24 hours a day, significantly improving production efficiency.
Strong flexibility: supports a variety of stacking designs and adapts to different specifications of packaging and products.
2. Practical application scenarios
(1) Food and beverage industry
In the food and beverage industry, large-load palletizing robots are widely used in palletizing operations for bottled water, beverages, beer and other products. For example, after a well-known beverage company introduced a large-load palletizing robot, it realized the automated palletizing of thousands of boxes of products per hour, which not only improved production efficiency but also reduced product loss during manual handling.
(2) Chemical and building materials industry
The chemical and building materials industries often need to handle heavy bagged or boxed materials such as fertilizers, cement, coatings, etc. Large-load palletizing robots can easily handle these high-weight and high-intensity handling tasks, ensuring operational safety and efficiency. A chemical company deployed large-load palletizing robots to increase palletizing efficiency by 30%, while reducing workers' labor intensity and safety risks.
With the continuous advancement of technology, large-load palletizing robots will play an important role in more fields. Its high load, high efficiency and intelligence will bring greater value to the manufacturing and logistics industries and promote the further development of industrial automation.
Latest News
GET A FREE QUOTE
If you are interested in our products and services, please contact us or leave us a message, we will serve you wholeheartedly
CONTACT US
Address : Shandong Tai'an Feicheng High-tech Development Zone

TikTok


YouTube

